- Home
- A-Z Catalogue
- Products
- Valves
- Cetop
- Manual Directional Valves
- Proportional Valves
- Poppet Valves
- High-Speed Linear Servo Valves
- All High-Speed Linear Servo Valves
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10 (With Fail-Safe)
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06 (With Fail-Safe)
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04 (With Fail-Safe)
- Cetop 5 (NG10) Direct Type High Speed Linear Servo Valves – LSVG-03
- Cetop 5 (NG10) OBE Type Direct Operated Linear Servo Valves – LSVG-03-EH
- Cetop 3 (NG6) OBE Type Direct Operated Linear Servo Valves – LSVG-01-EH
- Pumps
- Pressure control
- Flow Control Valves
- Pressure Control Valves
- All Pressure Control Valves
- Brake Valves
- Direct Relief Valve
- Low Noise Solenoid Controlled Relief Valves
- Low Noise Pilot Operated Relief Valves
- Pilot Operated Relief Valves
- Pressure reducing and relieving valves
- Pressure reducing and check valves
- Pressure control valves
- Remote Control Relief Valves
- Solenoid Controlled Relief Valves – BSG
- Solenoid Controlled Relief Valves – BST
- Unloading relief valves
- Check valves
- Environmental
- Valves
- Hydraulic Systems
- Power pack
- About Us
- Contact
- Blog
Top Solvent Free Lamination Machine Manufacturers?
Solvent Free Lamination is reshaping flexible packaging production through lower emissions, cleaner workplaces, and efficient adhesive application. It removes drying ovens from the process. Energy demand can also decrease. Yet equipment quality still matters.
Grand View Research reports that the global flexible packaging market reached approximately USD 261.6 billion in 2022. Its report projects continued growth through 2030. Smithers’ The Future of Global Flexible Packaging to 2028 also identifies sustainability and material efficiency as major investment drivers. These findings explain rising interest in solvent-free laminators. However, market forecasts differ by scope, currency, and packaging segment. Buyers should examine the methodology carefully.
Henkel packaging specialist Dr. Stefan Zepnik has emphasized, “Sustainability is no longer a niche topic; it is a business imperative.” That principle is visible on the factory floor. A modern machine may run without solvent ovens, reduce ventilation requirements, and support precise adhesive coating. Small details matter. Web tension, curing time, substrate compatibility, and operator training affect final performance.
This guide examines leading Solvent Free Lamination machine manufacturers and their practical strengths. It considers output speed, coating accuracy, automation, energy use, technical service, and lifecycle value. Some claims deserve skepticism. “Faster” does not always mean better. A high-speed line may create waste if setup control remains weak. Manufacturer brochures rarely show every limitation.
The right choice depends on film structure, production volume, adhesive chemistry, and regional support. Readers should compare test results, not slogans.
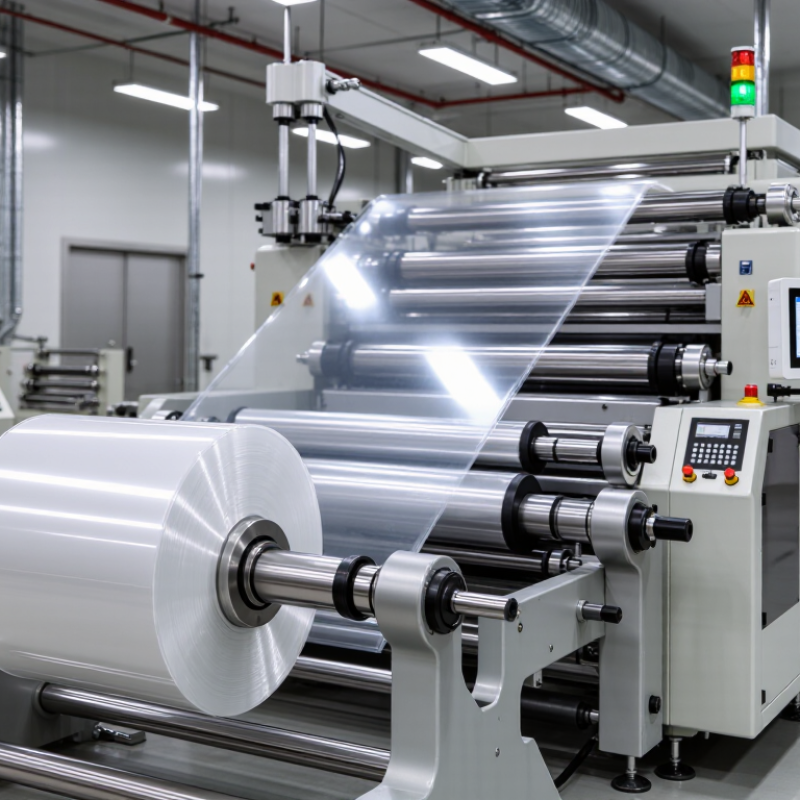
Table of Contents [Hide]
What Is a Solvent-Free Lamination Machine?
A solvent-free lamination machine bonds two or more flexible webs without evaporating liquid solvents. It usually applies a two-component polyurethane adhesive at low coat weights, often around 1–2 grams per square metre. The machine mixes, meters, and spreads the adhesive before pressing films together through a heated nip. There is no drying oven. That matters. Production areas can reduce solvent handling, exhaust demand, and related volatile organic compound emissions. The U.S. Environmental Protection Agency links VOC emissions with ground-level ozone formation, making emission control an important engineering concern.
The machine still needs careful control. Adhesive ratios, web tension, nip pressure, and temperature directly affect bond quality. A small mixing error may create weak edges or blocking during rewinding. Curing commonly takes one to several days, depending on the adhesive and film structure. Smithers’ flexible packaging market research projects global sales above US$300 billion by 2028, increasing demand for efficient converting equipment. Its findings also highlight lightweight structures and sustainability pressures. However, solvent-free technology is not automatically suitable for every job. High-speed lines can expose defects quickly. Operators need practical experience, clean calibration records, and regular peel-strength testing. I would not treat lower emissions as a complete sustainability score; electricity use, scrap, adhesive chemistry, and end-of-life recycling still require honest review.
Top Solvent Free Lamination Machine Manufacturers? - What Is a Solvent-Free Lamination Machine?
| Data Dimension | Typical Industry Information | Why It Matters |
|---|---|---|
| Machine Definition | A solvent-free lamination machine bonds flexible substrates with a 100% solids adhesive, normally without using an organic-solvent drying oven. | The process can reduce solvent emissions, drying energy, and solvent-recovery requirements. |
| Common Adhesive System | Two-component polyurethane adhesive consisting of a resin and a reactive hardener; some systems use a pre-mixed or single-component formulation. | Correct adhesive selection determines bond strength, curing behavior, food-contact suitability, and chemical resistance. |
| Typical Substrates | PET, BOPP, CPP, PE, cast polypropylene, aluminum foil, metallized films, paper, and selected coated films. | Substrate surface energy, thickness, heat sensitivity, and coating compatibility affect process stability. |
| Typical Web Width | Approximately 600–1,600 mm for many flexible-packaging production machines; custom widths are available for specialized lines. | The selected width should match the product portfolio, converting equipment, and required production capacity. |
| Typical Production Speed | Approximately 100–500 m/min, depending on adhesive chemistry, coating weight, substrate combination, curing time, and machine configuration. | The maximum rated speed is not always the practical operating speed for every laminate structure. |
| Adhesive Coating Method | Precision gravure coating, smooth-roll coating, or other metering systems designed for low-viscosity reactive adhesives. | Accurate metering helps control adhesive consumption, bond quality, and laminate appearance. |
| Typical Adhesive Coating Weight | Often about 1.0–2.5 g/m², although the required value depends on substrate roughness, ink coverage, film structure, and adhesive specification. | Using too little adhesive may cause poor bonding, while excessive coating increases cost and can extend curing time. |
| Mixing and Dosing | An automatic dosing unit meters the resin and hardener at a controlled ratio, commonly using separate heated tanks, pumps, and static or dynamic mixing components. | Stable ratio control is essential for complete reaction and consistent final bond performance. |
| Temperature Control | Heated adhesive tanks, hoses, metering components, and coating assemblies are commonly used to reduce viscosity and maintain uniform flow. | Temperature stability influences coating uniformity, metering accuracy, and machine start-up performance. |
| Laminating Nip | A pressure-controlled nip combines the coated web with the second substrate; the nip may be heated or temperature-controlled according to the adhesive and film structure. | Uniform pressure and alignment help prevent tunnels, wrinkles, bubbles, and incomplete contact. |
| Curing Requirement | The laminate generally requires post-curing, commonly from approximately 24 hours to several days, depending on adhesive chemistry and structure. | The laminate may not reach final bond strength immediately after leaving the machine. |
| Drying Oven Requirement | A conventional solvent-evaporation oven is generally not required, although the machine may include heated zones for adhesive and web-temperature control. | This can reduce line length and energy demand compared with solvent-based lamination systems. |
| Main Quality Controls | Web tension, coating weight, adhesive ratio, temperature, nip pressure, line speed, splice quality, and laminate appearance. | Monitoring these variables helps maintain repeatability across different production batches. |
| Typical Applications | Flexible food packaging, medical packaging, household products, personal-care packaging, industrial pouches, labels, and technical films. | The final application determines barrier, sealability, strength, appearance, and regulatory requirements. |
| Environmental Characteristics | No intentional solvent evaporation during normal lamination; volatile organic compound emissions are typically lower than with solvent-based systems. | Lower emissions may simplify workplace air management, but adhesive handling and ventilation are still required. |
| Key Selection Criteria | Working width, speed range, coating-weight accuracy, adhesive ratio control, substrate compatibility, tension control, curing capability, automation, and after-sales service. | A machine should be selected according to actual laminate structures and production targets rather than rated speed alone. |
| Manufacturer Evaluation Factors | Assess engineering experience, application testing, commissioning support, spare-parts availability, operator training, safety features, documentation, and compatibility with approved adhesive systems. | These factors influence ramp-up time, uptime, product consistency, and total cost of ownership. |
Note: Operating ranges are representative industry values. Actual performance depends on machine design, adhesive formulation, substrate structure, and production conditions.