

- Home
- A-Z Catalogue
- Products
- Valves
- Cetop
- Manual Directional Valves
- Proportional Valves
- Poppet Valves
- High-Speed Linear Servo Valves
- All High-Speed Linear Servo Valves
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10 (With Fail-Safe)
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06 (With Fail-Safe)
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04 (With Fail-Safe)
- Cetop 5 (NG10) Direct Type High Speed Linear Servo Valves – LSVG-03
- Cetop 5 (NG10) OBE Type Direct Operated Linear Servo Valves – LSVG-03-EH
- Cetop 3 (NG6) OBE Type Direct Operated Linear Servo Valves – LSVG-01-EH
- Pumps
- Pressure control
- Flow Control Valves
- Pressure Control Valves
- All Pressure Control Valves
- Brake Valves
- Direct Relief Valve
- Low Noise Solenoid Controlled Relief Valves
- Low Noise Pilot Operated Relief Valves
- Pilot Operated Relief Valves
- Pressure reducing and relieving valves
- Pressure reducing and check valves
- Pressure control valves
- Remote Control Relief Valves
- Solenoid Controlled Relief Valves – BSG
- Solenoid Controlled Relief Valves – BST
- Unloading relief valves
- Check valves
- Environmental
- Valves
- Hydraulic Systems
- Power pack
- About Us
- Contact
- Blog
Top 10 Types of DTF Transfer Film Rolls for Buyers
Choosing the right DTF Transfer Film Rolls (DTF Film) is more practical than simply comparing prices. Film affects ink release, powder bonding, color strength, washing durability, and production speed. A roll may look smooth under warehouse lighting, yet perform poorly on cotton after pressing.
DTF printing consultant Andy MacDougall states, “The film is part of the printing system, not just a disposable carrier.” This principle deserves attention. Printers should examine cold-peel, hot-peel, and warm-peel films separately. They should also consider matte and glossy surfaces, single-sided and double-sided coatings, stretch film, anti-static film, and films designed for fine-detail graphics. Those differences become visible on a black hoodie, especially around small white letters and thin outlines.
This guide introduces ten practical types of DTF film rolls for buyers. Each type has a useful place, but none is perfect. A low-cost film can reduce expenses. It can also create powder waste, weak adhesion, or uneven edges. That trade-off is easy to miss.
Check the coating consistency first.
Then test real garments.
A reliable evaluation should include roll width, thickness, release behavior, drying conditions, storage requirements, and compatibility with the printer and powder. Small test runs are wiser than immediate bulk purchasing. Humidity, curing temperature, and operator technique can change results significantly. Even experienced printers sometimes blame the film too quickly. The press settings may be the real problem.
The following overview focuses on observable performance, buyer experience, and production risks. It aims to help workshops choose with evidence, not attractive packaging or vague supplier claims.
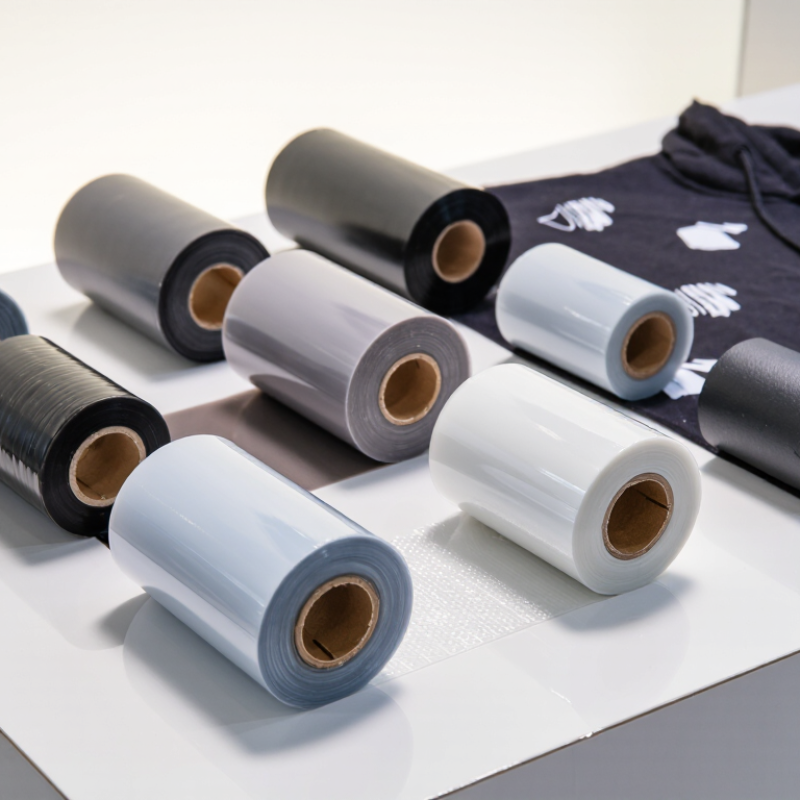
Table of Contents [Hide]
What DTF Transfer Film Rolls Are and How They Work
Top 10 Types of DTF Transfer Film Rolls for Buyers
DTF transfer film rolls are coated PET sheets used to move printed designs onto fabric. The printer places white and colored ink on the coated side, usually in a mirrored layout. Adhesive powder then bonds to the wet ink. Controlled heating melts the powder into a smooth, flexible layer. After curing, a heat press transfers the design to cotton, polyester, blends, and similar textiles.
Film performance depends on its coating, thickness, surface finish, and release behavior.
Common choices include cold-peel, hot-peel, instant-peel, glossy, matte, stretch, anti-static, high-release, textured, and low-temperature films.
Cold-peel film needs cooling before removal, while hot-peel film can be removed shortly after pressing. That difference affects production speed.
A matte surface can reduce glare, but it may feel slightly different on dark fabric.
Buyers should test film with their printer, ink, powder, and heat press settings. Check whether the roll feeds evenly without curling or static. Examine fine lettering under bright light.
Poor coating can cause pinholes, powder gaps, or weak edges after washing. A practical wash test should include several cycles, not one quick rinse.
Film specifications help, but they never replace a controlled sample test. I have seen promising samples fail after incorrect curing, and that remains an easy mistake to underestimate.
Temperature, pressure, dwell time, and peeling direction all deserve written records.