

- Home
- A-Z Catalogue
- Products
- Valves
- Cetop
- Manual Directional Valves
- Proportional Valves
- Poppet Valves
- High-Speed Linear Servo Valves
- All High-Speed Linear Servo Valves
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10 (With Fail-Safe)
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06 (With Fail-Safe)
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04 (With Fail-Safe)
- Cetop 5 (NG10) Direct Type High Speed Linear Servo Valves – LSVG-03
- Cetop 5 (NG10) OBE Type Direct Operated Linear Servo Valves – LSVG-03-EH
- Cetop 3 (NG6) OBE Type Direct Operated Linear Servo Valves – LSVG-01-EH
- Pumps
- Pressure control
- Flow Control Valves
- Pressure Control Valves
- All Pressure Control Valves
- Brake Valves
- Direct Relief Valve
- Low Noise Solenoid Controlled Relief Valves
- Low Noise Pilot Operated Relief Valves
- Pilot Operated Relief Valves
- Pressure reducing and relieving valves
- Pressure reducing and check valves
- Pressure control valves
- Remote Control Relief Valves
- Solenoid Controlled Relief Valves – BSG
- Solenoid Controlled Relief Valves – BST
- Unloading relief valves
- Check valves
- Environmental
- Valves
- Hydraulic Systems
- Power pack
- About Us
- Contact
- Blog
China Top Aluminum Tube Extrusions Manufacturers?
China has become a major sourcing base for Aluminum Tube Extrusions, serving construction, transport, furniture, and industrial equipment markets. However, choosing a leading manufacturer requires more than comparing factory photos or export figures. Real performance appears in the details.
Dr. J. Gilbert Kaufman, a respected aluminum metallurgy expert, emphasized a practical principle: “Composition and processing determine an aluminum alloy’s performance.” That principle matters when reviewing Chinese extrusion suppliers. A reliable manufacturer should explain alloy selection, billet quality, extrusion temperature, die design, and temper control. It should also provide traceable inspection records, dimensional reports, and material certificates. Small details count.
Look closely.
Experienced buyers should examine production capacity, minimum order quantities, tooling costs, surface finishing, packaging, and delivery consistency. Common options include 6061, 6063, and 6005A alloys, but the best choice depends on strength, corrosion resistance, wall thickness, and final use. A supplier may offer anodizing, powder coating, cutting, drilling, or CNC machining. These services can reduce handling between factories.
Still, no ranking is perfect. A large exporter may not provide the tightest tolerances. A smaller plant may deliver better technical support. Website claims also need verification through samples, drawings, factory audits, and independent testing. This guide compares China’s top Aluminum Tube Extrusions manufacturers through practical criteria, not advertising language. The evaluation remains imperfect, because supplier performance can change over time. That limitation deserves attention before signing any long-term agreement.
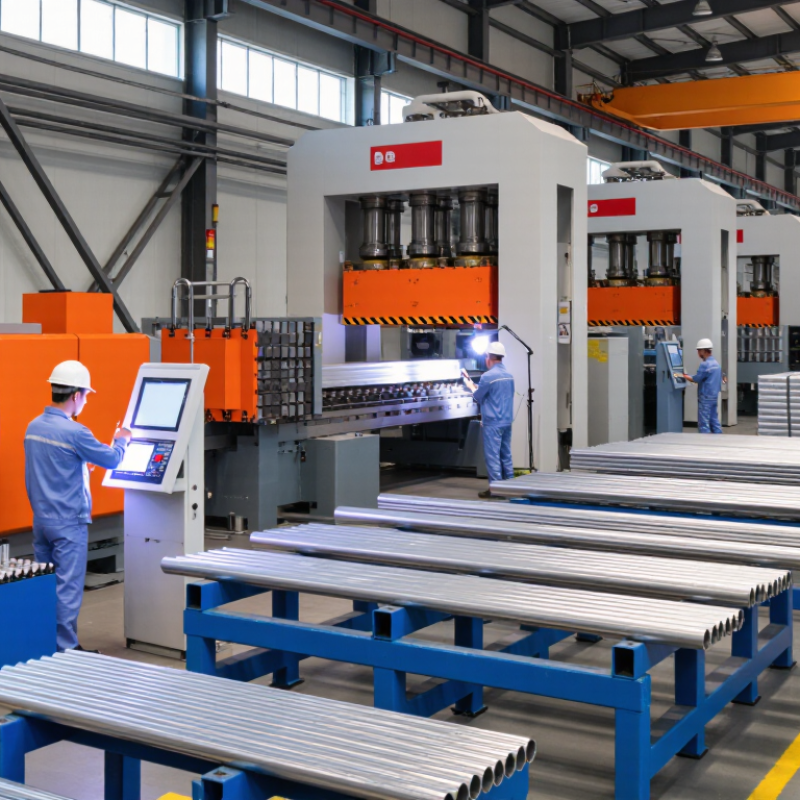
Table of Contents [Hide]
What Makes China’s Top Aluminum Tube Extrusion Manufacturers Stand Out?
China’s top aluminum tube extrusion manufacturers stand out through controlled production, not attractive catalogs alone. Their advantage begins with alloy selection, die design, and stable billet heating. Small temperature changes can create uneven wall thickness, especially in thin tubes. Experienced teams monitor press speed, cooling water, and dimensional tolerances during every run.
The International Aluminium Institute reports that recycling aluminum can save up to 95% of the energy required for primary production. Leading manufacturers therefore combine recycled content with strict chemical analysis. Spectrometers verify alloy composition before extrusion. Tensile tests, hardness checks, and leak testing then confirm performance. These steps support requirements under standards such as ASTM B221 and ISO 6892-1. Traceable inspection records also make quality claims more reliable.
Customization is another practical difference. Strong suppliers can adjust tooling for heat exchangers, furniture frames, transport parts, and industrial tubing. They discuss bend radius, surface finish, cut length, and packaging before production begins. The International Energy Agency identifies aluminum as responsible for roughly 3% of global carbon dioxide emissions, so energy efficiency now matters beside price. Some factories use closed-loop cooling and renewable electricity, though environmental claims still need verification. No supplier is perfect. A polished sample may hide weak communication, late tooling, or inconsistent batches. Buyer audits, pilot orders, and independent inspections remain necessary.
China Top Aluminum Tube Extrusions Manufacturers? - What Makes China’s Top Aluminum Tube Extrusion Manufacturers Stand Out?
| Evaluation Dimension | Relevant Data or Benchmark | What Leading Manufacturers Typically Demonstrate | Why It Matters for Buyers | Reference or Technical Basis |
|---|---|---|---|---|
| Common Tube Alloys | 6061, 6063, 6005A, and 6082 are widely used aluminum extrusion alloys. | They select the alloy according to the required balance of strength, corrosion resistance, machinability, surface quality, and weldability. | The correct alloy prevents over-specification, premature failure, and unnecessary material cost. | EN 573-3; ASTM B221; ISO 6362-2 |
| Typical Mechanical Strength | Depending on alloy and temper, extruded aluminum tubes commonly provide tensile strengths from approximately 150 to 330 MPa. | They provide documented mechanical-property results for each supplied alloy and temper instead of relying only on nominal alloy designations. | Verified strength data supports structural calculations and consistent product performance. | Values vary by alloy, temper, wall thickness, and applicable product standard. |
| Temper Control | Common tempers include O, H112, T5, and T6. | They control cooling and artificial-aging processes to achieve repeatable hardness and strength across production batches. | Incorrect temper control can cause dimensional instability, low strength, or inconsistent machining behavior. | ASTM B221; EN 515; ISO 2107 |
| Dimensional Tolerance | Commercial extrusion tolerances are normally defined by profile size, wall thickness, straightness, and applicable standard; tighter tolerances require special process control. | They confirm critical dimensions on production samples and clearly separate standard tolerances from specially negotiated tolerances. | Reliable tolerances reduce assembly problems, rework, and the need for extensive secondary machining. | EN 755-9; ASTM B221; ISO 6362-4 |
| Wall-Thickness Capability | Practical minimum wall thickness depends on alloy, tube diameter, profile complexity, extrusion ratio, and die design. | They review the design for metal flow, weld-line risk, die strength, and achievable wall uniformity before production. | Early engineering review helps avoid distortion, thin-wall defects, and unstable extrusion output. | Capability must be confirmed through a technical drawing and die-flow assessment. |
| Surface Finish Options | Common finishes include mill finish, anodizing, powder coating, polishing, and brushing. | They control surface preparation, cleaning, pretreatment, coating thickness, color consistency, and appearance inspection. | Stable surface quality is important for architectural, decorative, transport, and consumer-product applications. | ISO 7599 for anodized aluminum; ISO 2813 for coating gloss measurement. |
| Anodized Layer Thickness | Typical architectural anodizing classes are often specified from about 10 to 25 μm, depending on the application and local standard. | They specify the anodizing class, color tolerance, sealing requirements, and coating inspection method before mass production. | Correct layer thickness improves corrosion resistance and helps maintain a consistent appearance. | ISO 7599; project specifications may require different coating classes. |
| Cutting and Machining Accuracy | Cut length, drilling position, slot location, and end preparation are controlled according to the approved technical drawing. | They use calibrated equipment and documented first-article and in-process inspections for fabricated tube components. | Accurate fabrication reduces installation time and improves interchangeability in assemblies. | Acceptance limits should be stated on the drawing or purchase specification. |
| Quality Inspection System | Key inspections include chemical composition, dimensions, surface condition, mechanical properties, and packaging condition. | They maintain inspection records, calibration records, batch traceability, and corrective-action procedures. | Traceability makes it easier to identify nonconforming material and verify the source of each batch. | ISO 9001 provides a widely used framework for quality-management systems. |
| Material Certification | A material certificate may include alloy, temper, batch number, chemical composition, tensile strength, yield strength, and elongation. | They provide certificates that correspond to the actual shipment rather than generic certificates unrelated to the supplied batch. | Batch-specific documentation supports incoming inspection, compliance review, and project records. | EN 10204 Type 3.1 is commonly used when batch-specific inspection certification is required. |
| Corrosion-Resistance Consideration | Aluminum naturally forms a protective oxide film; corrosion performance still depends on alloy, environment, surface treatment, and contact with dissimilar metals. | They recommend suitable alloys and protective finishes for marine, industrial, outdoor, and humid environments. | Proper material selection reduces galvanic corrosion, staining, and premature surface deterioration. | Application-specific environmental testing and coating specifications may be required. |
| Tooling and Die Management | Extrusion die life depends on alloy, profile complexity, extrusion conditions, die material, maintenance, and production volume. | They use controlled die design, trial approval, maintenance records, and revision management for repeated orders. | Well-managed tooling improves profile consistency and reduces start-up waste and dimensional variation. | Die design and service life are project-specific and should be confirmed during technical review. |
| Production Flexibility | Manufacturers may support prototype runs, small batches, and larger recurring production orders, subject to equipment capacity. | They provide clear minimum-order quantities, sampling procedures, production lead times, and capacity information. | Flexible production helps buyers validate a design before committing to a large-volume order. | Actual capacity depends on billet size, press tonnage, profile dimensions, and finishing requirements. |
| Packaging and Export Protection | Common protection methods include plastic separation, moisture-resistant wrapping, reinforced cartons, pallets, and customized crating. | They adapt packaging to prevent scratches, bending, water exposure, and movement during international transport. | Proper packaging preserves the finished surface and reduces damage-related claims after delivery. | Packaging requirements should be agreed according to tube length, finish, loading method, and transport route. |