- Home
- A-Z Catalogue
- Products
- Valves
- Cetop
- Manual Directional Valves
- Proportional Valves
- Poppet Valves
- High-Speed Linear Servo Valves
- All High-Speed Linear Servo Valves
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10 (With Fail-Safe)
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06 (With Fail-Safe)
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04 (With Fail-Safe)
- Cetop 5 (NG10) Direct Type High Speed Linear Servo Valves – LSVG-03
- Cetop 5 (NG10) OBE Type Direct Operated Linear Servo Valves – LSVG-03-EH
- Cetop 3 (NG6) OBE Type Direct Operated Linear Servo Valves – LSVG-01-EH
- Pumps
- Pressure control
- Flow Control Valves
- Pressure Control Valves
- All Pressure Control Valves
- Brake Valves
- Direct Relief Valve
- Low Noise Solenoid Controlled Relief Valves
- Low Noise Pilot Operated Relief Valves
- Pilot Operated Relief Valves
- Pressure reducing and relieving valves
- Pressure reducing and check valves
- Pressure control valves
- Remote Control Relief Valves
- Solenoid Controlled Relief Valves – BSG
- Solenoid Controlled Relief Valves – BST
- Unloading relief valves
- Check valves
- Environmental
- Valves
- Hydraulic Systems
- Power pack
- About Us
- Contact
- Blog
China Top 10 Spunlace Machine Suppliers for Buyers?
China has become a serious sourcing base for spunlace production equipment. Its suppliers serve hygiene, medical, filtration, wipes, and household textile markets. Yet, a supplier list is not a purchasing decision. Factory scale, water-jet pressure, line speed, energy consumption, and after-sales response matter more than polished brochures.
Grand View Research valued the global nonwoven fabric market at approximately USD 53.78 billion in 2022. It also projected a 7.7% compound annual growth rate from 2023 to 2030. Smithers reports continued demand for spunlace materials, especially in wipes and hygiene applications. These figures explain the investment interest. They do not prove that every Spunlace Machine supplier offers equal performance.
As Dave Rousse, former president of INDA, has said, “Nonwovens are essential materials for modern life.” That observation is practical, not decorative. A modern line may run through several filtration stages, hydraulic entanglement zones, drying ovens, and winding units. Small design differences can affect fabric strength, moisture uniformity, and kilograms of water consumed per tonne.
This guide examines China’s top ten Spunlace Machine suppliers through measurable buyer concerns. The review considers operating references, automation depth, component quality, installation support, and spare-parts availability. Production claims still require verification. A factory visit is better than a sales presentation. Some rankings may remain debatable, because supplier data is not always published consistently. That is an important limitation. Reliable buyers should request trial samples, energy records, and customer references before signing any equipment contract.
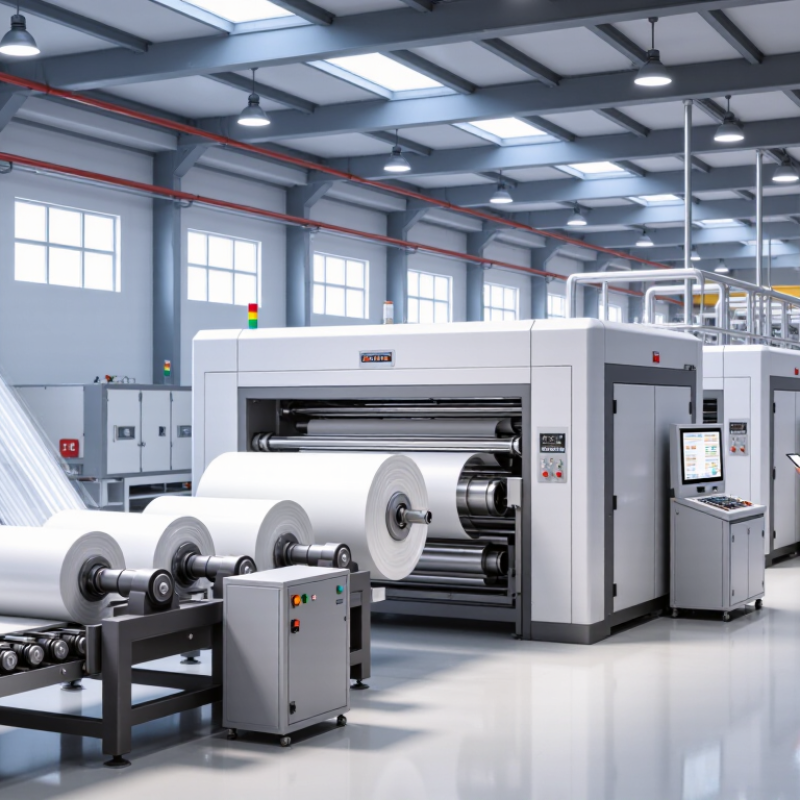
Table of Contents [Hide]
Spunlace Machines: Definition, Types, and Production Principles
Spunlace Machines: Definition, Types, and Production Principles
Spunlace machines produce nonwoven fabric by entangling fibers with fine, high-pressure water jets. Unlike woven equipment, they do not use yarn interlacing. A typical line includes fiber opening, web forming, cross-lapping, hydroentangling, dewatering, drying, and winding units. The process can handle viscose, polyester, cotton, and blended fibers. Results depend on fiber length, web uniformity, water pressure, and production speed.
Several machine types serve different needs. Flatbed systems suit stable, broad production lines. Drum-based systems can improve web support and pattern control. Some compact lines combine forming, entangling, and drying in limited space. From practical evaluations, operators should inspect nozzle alignment, filtration quality, water circulation, and control accuracy. Small defects matter. A blocked nozzle may create visible stripes across the fabric. Energy use and wastewater handling also affect long-term operating costs, not only the purchase price.
Tips: Ask for test production with your actual fiber blend. Check fabric strength, softness, absorbency, and weight variation. Request maintenance records and spare-part specifications. An impressive output figure may hide difficult cleaning work. That assumption needs checking. Buyers should also review operator training, safety systems, installation support, and documented performance data. A reliable assessment compares sample results with daily production conditions, because laboratory performance can differ from factory reality.
China Top 10 Spunlace Machine Suppliers for Buyers? - Spunlace Machines: Definition, Types, and Production Principles
| Profile | Machine Configuration | Effective Web Width | Design Line Speed | Typical Product GSM | Compatible Fibers | Production Principle | Indicative Output | Best Buyer Application |
|---|---|---|---|---|---|---|---|---|
| Profile 01 | Standard parallel-carded spunlace line | 1.6–2.5 m | 60–100 m/min | 30–80 g/m² | Viscose, polyester, polypropylene | Carded fibers are cross-lapped, then entangled by high-pressure water jets. | 250–850 kg/h | General wipes, hygiene materials, and entry-level nonwovens |
| Profile 02 | High-speed parallel-carded line | 2.5–3.5 m | 100–160 m/min | 40–100 g/m² | Viscose, polyester, cotton blends, bamboo fiber | Continuous web forming followed by multi-manifold hydroentanglement. | 700–1,700 kg/h | Large-volume wipes and disposable hygiene products |
| Profile 03 | Cross-lapped spunlace production line | 2.5–4.0 m | 50–110 m/min | 50–150 g/m² | Polyester, viscose, recycled fibers, cotton | Cross-lapping builds thickness and isotropic strength before water entanglement. | 650–1,900 kg/h | Furniture fabrics, filtration media, and technical substrates |
| Profile 04 | Hydroentangled line with recycled-fiber preparation | 2.0–3.2 m | 50–100 m/min | 35–100 g/m² | Recycled polyester, recycled cotton, regenerated cellulose | Opened and blended fibers form a web that is consolidated mechanically by water jets. | 450–1,250 kg/h | Sustainable wipes, cleaning cloths, and recycled nonwovens |
| Profile 05 | Air-through and spunlace composite line | 2.0–3.0 m | 40–90 m/min | 60–180 g/m² | Polyester, polypropylene, bicomponent fibers, viscose | A lofted web is thermally stabilized and then strengthened through hydroentanglement. | 400–1,050 kg/h | Absorbent cores, soft cover materials, and medical textiles |
| Profile 06 | Wetlaid and spunlace combination line | 2.0–3.2 m | 30–80 m/min | 25–90 g/m² | Cellulose pulp, viscose, cotton linters, short fibers | Fibers are dispersed in water, deposited as a sheet, and consolidated by water jets. | 300–950 kg/h | Flushable-style wipes, tissue-like materials, and absorbent products |
| Profile 07 | Heavyweight spunlace line | 2.5–4.0 m | 30–70 m/min | 100–250 g/m² | Polyester, polypropylene, viscose, aramid blends | Multiple web layers are bonded with controlled jet pressure and repeated consolidation zones. | 500–1,450 kg/h | Automotive interiors, roofing substrates, and industrial reinforcement |
| Profile 08 | Fine-fiber and soft-touch spunlace line | 1.8–3.0 m | 40–90 m/min | 20–70 g/m² | Fine-denier polyester, viscose, lyocell, bamboo fiber | Fine fibers are gently carded and entangled to create a smooth, drapable web. | 250–800 kg/h | Facial wipes, cosmetic pads, premium hygiene products, and soft lining |
| Profile 09 | Patterned or apertured spunlace line | 2.0–3.2 m | 40–100 m/min | 35–120 g/m² | Viscose, polyester, polypropylene, cellulose blends | Special jet patterns or forming surfaces create texture, apertures, or surface designs. | 350–1,150 kg/h | Decorative wipes, absorbent sheets, filtration layers, and embossed fabrics |
| Profile 10 | Integrated spunlace line with drying and rewinding | 2.5–3.5 m | 70–130 m/min | 30–120 g/m² | Viscose, polyester, polypropylene, recycled and bio-based fibers | Web formation, hydroentanglement, water recovery, drying, inspection, and roll winding are integrated. | 650–1,600 kg/h | Export-oriented factories requiring automation and stable roll quality |