- Home
- A-Z Catalogue
- Products
- Valves
- Cetop
- Manual Directional Valves
- Proportional Valves
- Poppet Valves
- High-Speed Linear Servo Valves
- All High-Speed Linear Servo Valves
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10 (With Fail-Safe)
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06 (With Fail-Safe)
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04 (With Fail-Safe)
- Cetop 5 (NG10) Direct Type High Speed Linear Servo Valves – LSVG-03
- Cetop 5 (NG10) OBE Type Direct Operated Linear Servo Valves – LSVG-03-EH
- Cetop 3 (NG6) OBE Type Direct Operated Linear Servo Valves – LSVG-01-EH
- Pumps
- Pressure control
- Flow Control Valves
- Pressure Control Valves
- All Pressure Control Valves
- Brake Valves
- Direct Relief Valve
- Low Noise Solenoid Controlled Relief Valves
- Low Noise Pilot Operated Relief Valves
- Pilot Operated Relief Valves
- Pressure reducing and relieving valves
- Pressure reducing and check valves
- Pressure control valves
- Remote Control Relief Valves
- Solenoid Controlled Relief Valves – BSG
- Solenoid Controlled Relief Valves – BST
- Unloading relief valves
- Check valves
- Environmental
- Valves
- Hydraulic Systems
- Power pack
- About Us
- Contact
- Blog
How to Choose a Rubber Deflashing Machine
Choosing a Rubber Deflashing Machine starts with the parts you actually produce, not the most impressive machine specification. Rubber compound, part size, flash thickness, and component geometry all affect how reliably excess material can be removed. A small molded seal with thin flash may need a different process from a thick, complex automotive component. Details matter.
Compare mechanical trimming and cryogenic deflashing against your part requirements. Mechanical systems can suit accessible flash, while cryogenic processes may help with intricate shapes and hard-to-reach edges. Neither option is automatically best. Ask suppliers to process representative samples, then inspect the results for surface damage, leftover flash, and consistency across a batch. One successful sample is useful, but repeatability matters more.
Consider practical operating needs, too: expected throughput, loading method, floor space, noise, maintenance access, and operator training. Review how the machine handles different part sizes and compound variations. A low purchase price can be misleading if setup is difficult or routine cleaning takes longer than expected. Check service support and spare-parts availability before committing. Small omissions add up.
Real production is rarely as neat as a brochure suggests. Your parts may vary. That is worth planning for. Keep room for a trial run, and record the settings that produce acceptable results. The right Rubber Deflashing Machine should match your components, workflow, and quality expectations, while leaving enough flexibility for changes you have not encountered yet.
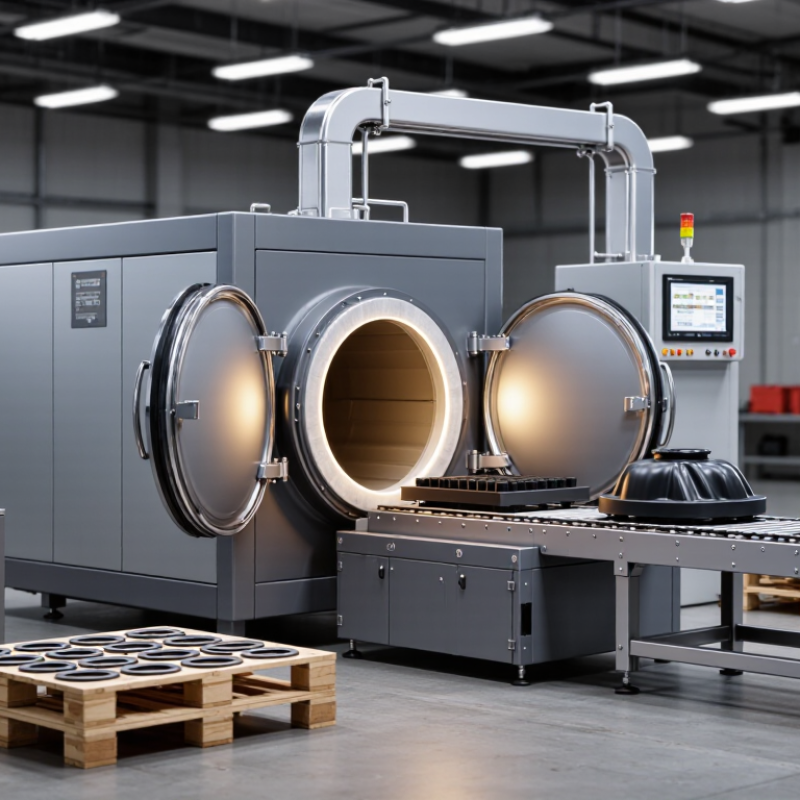
Table of Contents [Hide]
Identify the Rubber Parts and Flash Removal Requirements
Before choosing a rubber deflashing machine, identify the part’s material, shape, and flash location. EPDM seals, silicone gaskets, and nitrile O-rings behave differently under impact and abrasion. Record hardness, wall thickness, delicate edges, and any holes or grooves that must stay open. A thin fin along a mould seam is not the same problem as a thick gate remnant. Small details matter.
Define the acceptable result with a drawing or sample, not just “clean.” Note the maximum flash thickness, critical dimensions, surface-finish limits, and whether parts can tolerate tumbling or contact with media. The International Rubber Study Group’s World Rubber Industry Outlook 2024 estimated global rubber demand at about 31.4 million tonnes for 2024. That broad figure signals a large, varied industry; it does not tell you how a specific seal will respond to deflashing. Test real parts.
Ask the supplier to process representative parts from different cavities and production runs. Inspect edges under magnification, then check dimensions and functional fit. For thin diaphragms, even slight edge damage may matter. For robust moulded components, a higher-throughput process may be acceptable. I would not rely on one perfect sample; production variation can change the result. Keep samples, settings, and inspection records together.