- Home
- A-Z Catalogue
- Products
- Valves
- Cetop
- Manual Directional Valves
- Proportional Valves
- Poppet Valves
- High-Speed Linear Servo Valves
- All High-Speed Linear Servo Valves
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10 (With Fail-Safe)
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06 (With Fail-Safe)
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04 (With Fail-Safe)
- Cetop 5 (NG10) Direct Type High Speed Linear Servo Valves – LSVG-03
- Cetop 5 (NG10) OBE Type Direct Operated Linear Servo Valves – LSVG-03-EH
- Cetop 3 (NG6) OBE Type Direct Operated Linear Servo Valves – LSVG-01-EH
- Pumps
- Pressure control
- Flow Control Valves
- Pressure Control Valves
- All Pressure Control Valves
- Brake Valves
- Direct Relief Valve
- Low Noise Solenoid Controlled Relief Valves
- Low Noise Pilot Operated Relief Valves
- Pilot Operated Relief Valves
- Pressure reducing and relieving valves
- Pressure reducing and check valves
- Pressure control valves
- Remote Control Relief Valves
- Solenoid Controlled Relief Valves – BSG
- Solenoid Controlled Relief Valves – BST
- Unloading relief valves
- Check valves
- Environmental
- Valves
- Hydraulic Systems
- Power pack
- About Us
- Contact
- Blog
How to Choose Stainless Steel Buttons for Global Sourcing?
Choosing Stainless Steel Buttons for global sourcing requires more than comparing catalog photographs. A bright surface may hide weak plating, sharp edges, or inconsistent threading. The button must suit the garment, production method, destination market, and care instructions. Small details matter.
Apparel hardware specialist Michael J. Kaye states, “A button is small, but its failure can define the whole garment.” His observation reflects practical factory experience. Buyers should request material specifications, dimensional drawings, finish samples, and recent inspection records. Stainless steel grades deserve careful attention. Grade 304 often supports general apparel use, while Grade 316 may offer stronger resistance in humid or salty environments. However, the correct grade depends on design, exposure, cost, and supplier capability.
Ask for corrosion testing, pull-off strength results, and nickel-release documentation when relevant. Check the button by hand. Run a fingernail around its rim. Inspect the shank, holes, back, and polishing marks under direct light. A sample can look perfect, yet bulk production may vary. That is the uncomfortable part. Sampling alone is not enough. A written quality limit, approved reference sample, and pre-shipment inspection create better control.
Global sourcing also requires clear communication. Confirm packaging, carton quantities, labeling, lead times, replacement policies, and factory audit records. Do not select the lowest quotation automatically. An inexpensive button can create rework, customer complaints, or damaged brand trust. Stainless Steel Buttons should balance durability, appearance, compliance, and production reliability. The best choice is rarely the most decorative one. It is the one that performs consistently after thousands of garments leave the factory.
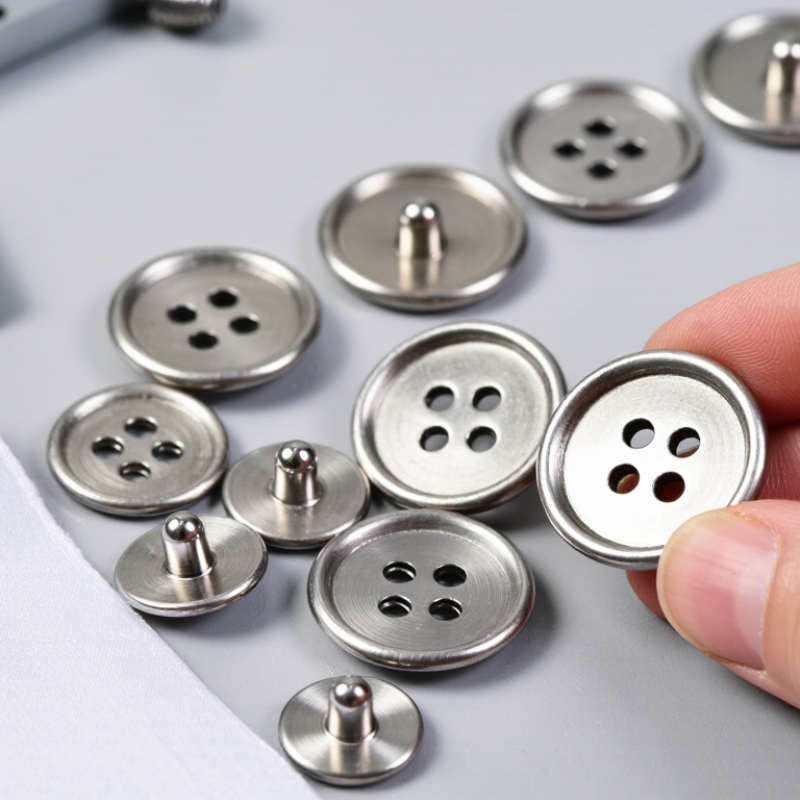
Table of Contents [Hide]
Define Button Requirements: Size, Shank Type, Load, Finish, and End Use
Choosing stainless steel buttons for global sourcing starts with a precise requirement sheet. Specify diameter, thickness, hole spacing, and shank type before requesting samples. A 15 mm button may suit a lightweight shirt, while a larger shank button needs stronger fabric support. End use changes everything: workwear needs impact resistance, children's clothing needs secure attachment, and outerwear needs better corrosion protection. The International Stainless Steel Forum reported 58.4 million tonnes of global stainless steel production in 2023, showing the scale of available material, but not every grade suits apparel hardware.
Define the expected load with a real test method. ASTM D4846 measures the resistance of fasteners pulled from fabric, helping suppliers compare button attachment strength. Test the complete system, including thread, fabric, washer, and shank. The button alone can pass while the garment fails. That detail is often missed. Record the stainless steel grade, surface treatment, coating thickness, and salt-spray results where relevant. ISO 9227 can support corrosion testing, although its laboratory conditions do not perfectly represent daily wear.
Finish selection should match the garment’s touch, cleaning process, and visual life. Brushed surfaces hide fingerprints better, while mirror finishes reveal tiny scratches under store lighting. Ask for color consistency across production lots. I once treated “silver” as a sufficient finish description; it was not. Require approved samples, dimensional tolerances, pull-test records, and packaging details. Review these documents before bulk production, not after a shipment arrives.