- Home
- A-Z Catalogue
- Products
- Valves
- Cetop
- Manual Directional Valves
- Proportional Valves
- Poppet Valves
- High-Speed Linear Servo Valves
- All High-Speed Linear Servo Valves
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10 (With Fail-Safe)
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06 (With Fail-Safe)
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04 (With Fail-Safe)
- Cetop 5 (NG10) Direct Type High Speed Linear Servo Valves – LSVG-03
- Cetop 5 (NG10) OBE Type Direct Operated Linear Servo Valves – LSVG-03-EH
- Cetop 3 (NG6) OBE Type Direct Operated Linear Servo Valves – LSVG-01-EH
- Pumps
- Pressure control
- Flow Control Valves
- Pressure Control Valves
- All Pressure Control Valves
- Brake Valves
- Direct Relief Valve
- Low Noise Solenoid Controlled Relief Valves
- Low Noise Pilot Operated Relief Valves
- Pilot Operated Relief Valves
- Pressure reducing and relieving valves
- Pressure reducing and check valves
- Pressure control valves
- Remote Control Relief Valves
- Solenoid Controlled Relief Valves – BSG
- Solenoid Controlled Relief Valves – BST
- Unloading relief valves
- Check valves
- Environmental
- Valves
- Hydraulic Systems
- Power pack
- About Us
- Contact
- Blog
How to Choose Arc Welding Equipment in 2026?
Choosing Arc Welding Equipment in 2026 starts with the work, not the product label. Consider the metals, thicknesses, joint positions, and expected hours of use. A machine suited to thin sheet metal may struggle with heavier sections or long production runs. Match the welding process to your typical jobs, then confirm the machine supports it. Small details matter.
A compact inverter may be easier to move between a workshop and a jobsite. Still, portability alone does not make a machine a good fit. Check its input power, output range, duty cycle, and compatibility with your available electrodes or wire. Read the manufacturer’s specifications carefully. If a rating is unclear, ask the supplier or a qualified welding professional before buying.
The rest of the setup deserves attention too. A suitable helmet, gloves, cables, and clamps can affect comfort and workflow. Confirm that replacement parts and technical support are available where you work. For safety, follow the equipment manual and use appropriate protective measures for your materials and workspace. No single machine is best for every welder. Even an experienced buyer can overlook a limitation when focusing on price or headline amperage. Take time to compare real job requirements with the specifications. The right choice should fit your work today, with enough flexibility for the jobs you can reasonably expect tomorrow.
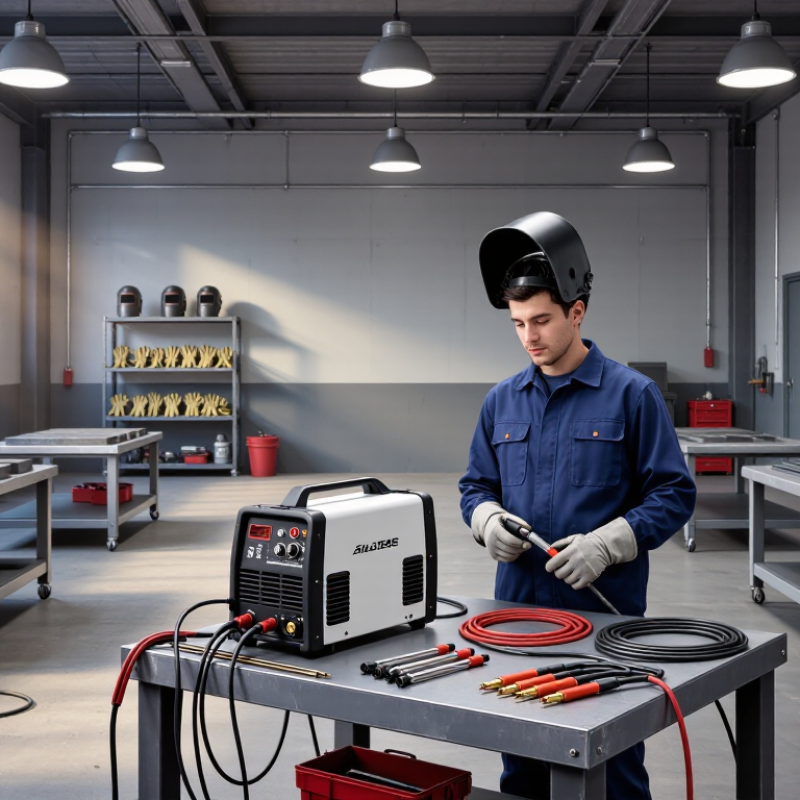
Table of Contents [Hide]
Identify Your Welding Applications and Materials
Before choosing arc welding equipment, list the actual jobs: repair work outdoors, thin-sheet fabrication, or repeated production welds. Record material, thickness, joint type, welding position, and available power. A portable stick welder can suit field repairs, while shop work may favor wire-feed equipment. Details matter.
Material use provides helpful context, but not a machine specification. The World Steel Association’s World Steel in Figures 2025 reports 1,882.6 million tonnes of crude steel production in 2024. That scale reflects steel’s role in fabrication; it does not mean every steel job needs the same process. The American Welding Society’s 2023 workforce outlook projected demand for up to 360,000 welding professionals by 2027. Training and straightforward controls can therefore matter alongside output.
For mild steel, compare stick, flux-cored, and gas-shielded wire processes against site conditions and cleanup needs. Stainless steel may call for careful heat control to limit distortion and discoloration. Aluminum needs compatible wire, polarity, and shielding gas; thin sections can demand steady control. A machine suitable for steel repairs may disappoint on thin aluminum. Check duty cycle and input power against real operating conditions, not just the largest amperage printed on a specification sheet.
How to Choose Arc Welding Equipment in 2026? — Identify Your Welding Applications and Materials
| Welding Process | Typical Applications | Common Materials | Typical Power Source and Output | Polarity and Shielding | Equipment to Consider | Key Selection Checks |
|---|---|---|---|---|---|---|
| SMAW (Stick) | Outdoor repair, construction, maintenance, and jobs where portability and simple setup matter. | Carbon steel, low-alloy steel, stainless steel, and some cast irons with suitable electrodes. | Constant-current power source; commonly about 30–300 A, depending on electrode size and work. | AC or DC may be used, depending on the electrode. DC electrode-positive is common, but electrode requirements vary. | Inverter or transformer-rectifier power source, electrode holder, work clamp, and leads. | Check the electrode’s recommended current and polarity, available input power, open-circuit voltage, and duty cycle. |
| GMAW (MIG/MAG) | Shop fabrication, vehicle repair, and production work requiring relatively high deposition rates and continuous wire feeding. | Carbon steel, stainless steel, and aluminum with the appropriate wire, shielding gas, and setup. | Usually a constant-voltage source with a wire feeder; commonly about 30–400 A across equipment sizes. | Typically DCEP. Uses shielding gas; gas composition depends on the wire and material. | Power source, wire feeder, welding gun, gas regulator/flowmeter, and suitable wire-feed rolls and liner. | Match output and duty cycle to material thickness and production rate. Confirm input supply, wire diameter range, and gas availability. |
| FCAW (Flux-Cored) | Structural fabrication, heavier fabrication, and outdoor work where higher deposition or improved tolerance to drafts is useful. | Primarily carbon and low-alloy steels; stainless flux-cored wires are also available for suitable applications. | Usually a constant-voltage source with a wire feeder; commonly about 100–500 A, depending on wire and application. | Gas-shielded wires commonly use DCEP. Self-shielded wires may use DCEP or DCEN; follow the wire specification. | Power source, feeder, gun, and either shielding-gas equipment or a setup for self-shielded wire. | Identify whether the wire is gas-shielded or self-shielded, verify polarity, and check wire compatibility and fume-control needs. |
| GTAW (TIG) | Precision work, thin sections, clean welds, and applications where careful control of the weld pool is important. | Carbon steel, stainless steel, aluminum, copper alloys, and other weldable metals with suitable procedures. | Constant-current source; commonly about 5–300 A, with specialized equipment available outside this range. | DCEN is common for steels and many other metals. AC is commonly used for aluminum and magnesium. Inert shielding gas is required. | TIG-capable power source, torch, gas regulator/flowmeter, tungsten electrodes, and filler rods where needed. | Check low-current control for thin material, AC capability for aluminum, torch cooling requirements, and gas coverage. |
| SAW (Submerged Arc) | High-volume, mechanized welding of long seams, large vessels, beams, and heavy plate. | Most commonly carbon and low-alloy steels; consumable combinations must suit the base metal and procedure. | High-output constant-voltage or constant-current systems; commonly about 200–1,000 A, depending on configuration. | DC electrode-positive is common; AC and other configurations are used for particular setups. Flux covers the arc during welding. | High-capacity power source, wire-feed system, flux delivery and recovery equipment, and a mechanized carriage or positioner. | Confirm automation needs, joint access, flux handling, power capacity, travel speed, and duty cycle for continuous operation. |
Selection note: Current ranges are broad examples, not machine ratings or welding procedure specifications. Choose equipment based on the material, thickness, joint design, required process, input power, duty cycle, and applicable welding code. Always follow the electrode or wire manufacturer’s recommendations and the qualified welding procedure.