- Home
- A-Z Catalogue
- Products
- Valves
- Cetop
- Manual Directional Valves
- Proportional Valves
- Poppet Valves
- High-Speed Linear Servo Valves
- All High-Speed Linear Servo Valves
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10 (With Fail-Safe)
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06 (With Fail-Safe)
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04 (With Fail-Safe)
- Cetop 5 (NG10) Direct Type High Speed Linear Servo Valves – LSVG-03
- Cetop 5 (NG10) OBE Type Direct Operated Linear Servo Valves – LSVG-03-EH
- Cetop 3 (NG6) OBE Type Direct Operated Linear Servo Valves – LSVG-01-EH
- Pumps
- Pressure control
- Flow Control Valves
- Pressure Control Valves
- All Pressure Control Valves
- Brake Valves
- Direct Relief Valve
- Low Noise Solenoid Controlled Relief Valves
- Low Noise Pilot Operated Relief Valves
- Pilot Operated Relief Valves
- Pressure reducing and relieving valves
- Pressure reducing and check valves
- Pressure control valves
- Remote Control Relief Valves
- Solenoid Controlled Relief Valves – BSG
- Solenoid Controlled Relief Valves – BST
- Unloading relief valves
- Check valves
- Environmental
- Valves
- Hydraulic Systems
- Power pack
- About Us
- Contact
- Blog
How to Choose a Memory Foam Core Pillow Filling Machine?
Choosing a Memory Foam Core Pillow Filling Machine starts with the foam, not the brochure. Core diameter, density, cut length, and daily output all affect how reliably a machine feeds and shapes material. Grand View Research estimated the global memory foam mattress market at USD 5.9 billion in 2022 and projected a 7.4% compound annual growth rate from 2023 to 2030. That report covers mattresses, not pillow-filling equipment, so it signals activity in a related market—not guaranteed demand for any machine.
Look closely at the working details. Can the feeder handle your foam’s firmness without tearing it? Does the cutting system produce consistent lengths? Ask for a trial using your own material, then inspect the cores for uneven edges and compression. Small details matter. W. Edwards Deming’s quality principle, “Quality is everyone’s responsibility,” is a useful reminder: stable results depend on the machine, its setup, and the operator. Compare actual throughput, changeover time, cleaning access, spare-part availability, and service support—not just the advertised speed. Foam is unforgiving. A machine that runs quickly but creates waste may cost more in practice. One limitation deserves honest attention: published market data rarely measures pillow-core machine demand directly. Treat forecasts as context, verify supplier claims with test runs, and choose equipment around your own production conditions.
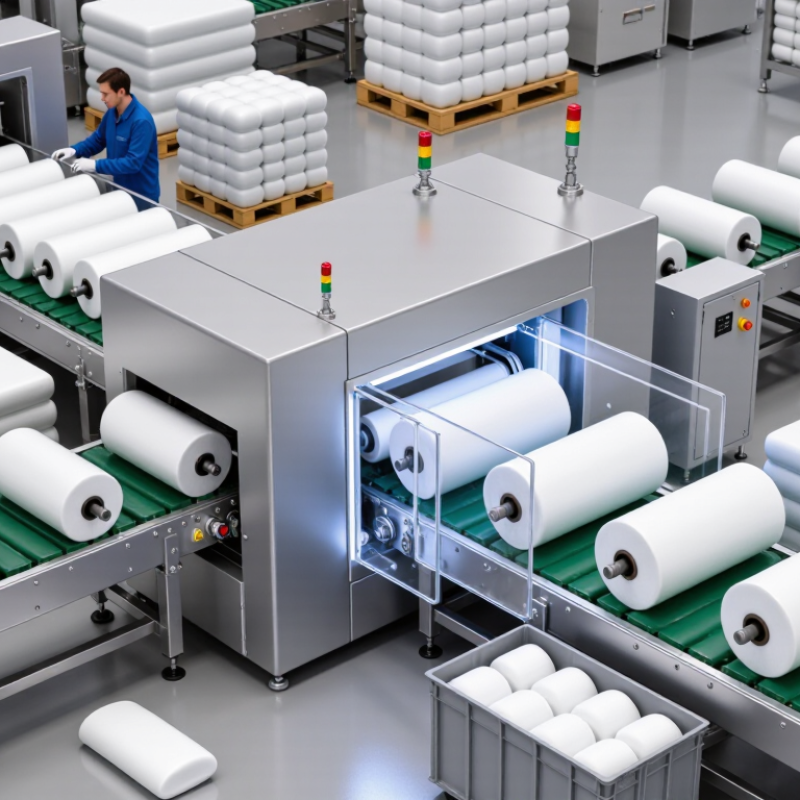
Table of Contents [Hide]
Measure Foam Density with ISO 845 and IFD with ASTM D3574
Before choosing a memory foam core pillow filling machine, test the foam itself. ISO 845:2006 defines how to determine apparent density from mass and volume. Record the result in kg/m³ for each foam batch. Density helps estimate material use and feeding consistency, but it does not tell you how firm a pillow will feel. Small differences matter.
Measure firmness separately using ASTM D3574. Its IFD procedures quantify the force needed to indent foam to specified levels, commonly including 25% indentation. Record the test conditions and force in newtons; otherwise, results from different samples may not be comparable. Measure, don’t guess. A higher IFD can mean greater resistance during compression, so check whether the machine’s feed system handles the foam without excessive crushing or uneven filling.
Use both measurements when comparing machines: density informs expected foam mass per core, while IFD helps characterize resistance during handling. Ask suppliers for feed-rate trials using your own tested foam, not just a generic sample. Watch for uneven pieces and rebound after filling. Not perfect, though. Foam temperature, aging, and cutting can shift results, so document them alongside each test. ISO 845 and ASTM D3574 provide useful technical methods, but your production checks still need to reflect the pillow design.
How to Choose a Memory Foam Core Pillow Filling Machine? - Measure Foam Density with ISO 845 and IFD with ASTM D3574
Use the measurements below to connect filling-machine performance with finished-foam quality. The sample results are illustrative examples, not product specifications or universal acceptance limits.
| Evaluation Area | Measurement or Check | Example Data | What to Look for in the Machine | Interpretation |
|---|---|---|---|---|
| Apparent foam density | Determine mass per volume using ISO 845. Density = mass ÷ volume. | Example coupon: 300 × 150 × 80 mm = 0.0036 m³. Mass = 180 g (0.180 kg). Density = 0.180 ÷ 0.0036 = 50.0 kg/m³. | Check that the system meters the required components consistently and supports the production process used to achieve the specified foam density. | ISO 845 describes a density measurement method; it does not prescribe a suitable density for every pillow core. |
| Density comparison across samples | Measure separate, representative specimens using the same documented sampling and test procedure. | Illustrative results: Sample A, 180 g → 50.0 kg/m³; Sample B, 177 g → 49.2 kg/m³; Sample C, 184 g → 51.1 kg/m³. Each specimen volume: 0.0036 m³. | Ask for repeatable component metering, clear calibration procedures, and production records that can be linked to each batch. | Compare results with the buyer’s own product specification and sampling plan, rather than treating these example values as a standard tolerance. |
| Indentation Force Deflection (IFD) | Measure according to ASTM D3574, Test B1, using the selected test configuration and a documented indentation level. | Illustrative result: 12.0 lbf at 25% indentation for a tested specimen. Record the specimen details, conditioning, test setup, indentation level, and force. | Confirm that the machine can deliver consistent formulation and process conditions. Request trial runs using the intended foam system and pillow-core design. | IFD depends on formulation, specimen preparation, conditioning, and test setup. A single IFD value is not a universal pillow-comfort rating. |
| Fill-mass repeatability | Weigh a series of filled cores at the intended production settings and record each result. | Record the target mass, individual core masses, mean, range, and test conditions for each trial. | Evaluate dosing accuracy, control stability, recipe settings, and the ease of checking or recalibrating the metering system. | Set the acceptance limit from the finished-product specification; ISO 845 and ASTM D3574 do not set a filling-machine mass tolerance. |
| Mixing and process control | Review component ratio, flow or delivery settings, operating records, and consistency between trial runs. | Document the formulation ratio and operating settings used for each foam batch; verify them against the foam-system supplier’s process instructions. | Look for suitable metering range, controllable delivery, repeatable mixing, and accessible records for troubleshooting. | The machine supports process consistency, but foam chemistry and curing conditions also influence density and IFD. |
| Pillow-core compatibility | Run a production-representative trial with the intended core shape, mold or filling arrangement, and production cycle. | Record core dimensions, fill mass, visible defects, cycle time, and results from density and IFD testing. | Check that the equipment can handle the required core geometry, production rate, material delivery, cleaning routine, and operator workflow. | Approve equipment using representative trials and the buyer’s quality criteria, not machine capacity alone. |
Testing note: Use separate specimens when required by the applicable procedures. Follow the current editions of ISO 845 and ASTM D3574 for specimen preparation, conditioning, apparatus, and reporting. The example coupon dimensions and test results above are for illustration only.