- Home
- A-Z Catalogue
- Products
- Valves
- Cetop
- Manual Directional Valves
- Proportional Valves
- Poppet Valves
- High-Speed Linear Servo Valves
- All High-Speed Linear Servo Valves
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10 (With Fail-Safe)
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06 (With Fail-Safe)
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04 (With Fail-Safe)
- Cetop 5 (NG10) Direct Type High Speed Linear Servo Valves – LSVG-03
- Cetop 5 (NG10) OBE Type Direct Operated Linear Servo Valves – LSVG-03-EH
- Cetop 3 (NG6) OBE Type Direct Operated Linear Servo Valves – LSVG-01-EH
- Pumps
- Pressure control
- Flow Control Valves
- Pressure Control Valves
- All Pressure Control Valves
- Brake Valves
- Direct Relief Valve
- Low Noise Solenoid Controlled Relief Valves
- Low Noise Pilot Operated Relief Valves
- Pilot Operated Relief Valves
- Pressure reducing and relieving valves
- Pressure reducing and check valves
- Pressure control valves
- Remote Control Relief Valves
- Solenoid Controlled Relief Valves – BSG
- Solenoid Controlled Relief Valves – BST
- Unloading relief valves
- Check valves
- Environmental
- Valves
- Hydraulic Systems
- Power pack
- About Us
- Contact
- Blog
China Best All Aluminum Interior Doors for Global Buyers?
China Best All-Aluminum Interior Doors for Global Buyers?
All-Aluminum Interior Doors are becoming a practical choice for modern homes, hotels, offices, and apartments. Chinese manufacturers now offer slim frames, concealed hinges, sliding systems, and custom finishes for international projects. The appeal is clear. Aluminum resists moisture, insects, and everyday impact better than many wood-based materials. It also supports clean lines and large glass panels.
Daniel Wu, an architectural door systems consultant with more than fifteen years of project experience, explains, “A dependable aluminum door should open smoothly, close quietly, and keep its shape after years of use.” That simple standard matters. Buyers should inspect alloy grades, wall thickness, hardware quality, coating performance, and assembly tolerances. A beautiful sample proves very little by itself. Factory audits, test reports, and completed project references offer stronger evidence.
China can provide competitive pricing and flexible customization. However, low cost should not become the only buying signal. Some doors look refined in photographs but feel weak at the handle. Others have impressive finishes but poor seals or uneven gaps. That is an uncomfortable reality. Even experienced buyers can miss small details during remote purchasing. Clear drawings, approved samples, packaging checks, and pre-shipment inspections reduce avoidable problems. Local installation conditions also deserve attention, especially wall accuracy and floor levels. This guide examines what global buyers should compare before selecting All-Aluminum Interior Doors from China. The goal is not to praise every supplier. It is to identify reliable performance, transparent communication, and value that remains convincing after installation.
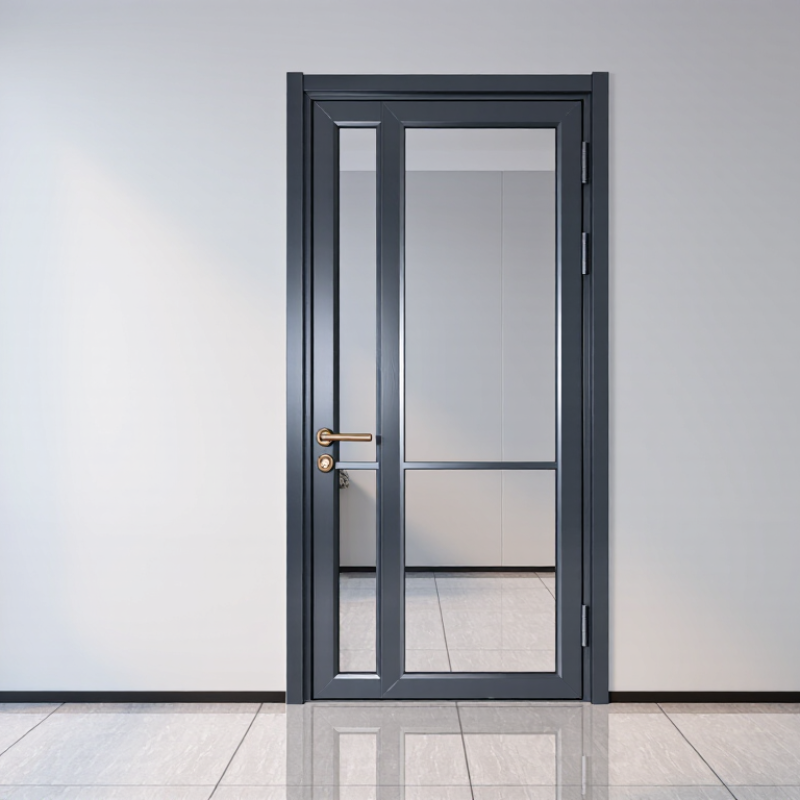
Table of Contents [Hide]
All-Aluminum Interior Doors: 6063-T5 Profiles and Core Materials
China Best All Aluminum Interior Doors for Global Buyers?
All-aluminum interior doors depend on two technical choices: 6063-T5 profiles and the core material. The 6063 alloy supports clean extrusion and smooth surface finishing. T5 tempering improves practical strength after controlled cooling. These profiles suit door stiles, rails, frames, and slim glazing borders. Built to fit.
Profile thickness should match the door size, hardware load, and opening frequency. A thicker section is not always better. It can increase weight and complicate installation. Anodizing resists surface wear, while powder coating offers wider color options. Surface preparation still matters. Poor preparation can cause uneven coverage or early peeling.
The core controls much of the door’s real performance. Aluminum honeycomb keeps the panel light and stable, but sound reduction may be limited. Mineral wool can improve acoustic and fire performance when the complete door assembly is tested. Other engineered cores may support impact resistance or moisture control.
Core claims should never stand alone. Buyers need test reports for the finished door, frame, seals, and hardware. In my experience, small gaps around the frame often reduce performance more than the selected core. That detail is easy to overlook.
Ask for dimensional tolerances, corner-joint samples, flatness data, and installation guidance before approving production. A sample exposed to repeated opening cycles can reveal weaknesses that drawings miss. No system is perfect. Careful verification remains essential.