- Home
- A-Z Catalogue
- Products
- Valves
- Cetop
- Manual Directional Valves
- Proportional Valves
- Poppet Valves
- High-Speed Linear Servo Valves
- All High-Speed Linear Servo Valves
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10 (With Fail-Safe)
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06 (With Fail-Safe)
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04 (With Fail-Safe)
- Cetop 5 (NG10) Direct Type High Speed Linear Servo Valves – LSVG-03
- Cetop 5 (NG10) OBE Type Direct Operated Linear Servo Valves – LSVG-03-EH
- Cetop 3 (NG6) OBE Type Direct Operated Linear Servo Valves – LSVG-01-EH
- Pumps
- Pressure control
- Flow Control Valves
- Pressure Control Valves
- All Pressure Control Valves
- Brake Valves
- Direct Relief Valve
- Low Noise Solenoid Controlled Relief Valves
- Low Noise Pilot Operated Relief Valves
- Pilot Operated Relief Valves
- Pressure reducing and relieving valves
- Pressure reducing and check valves
- Pressure control valves
- Remote Control Relief Valves
- Solenoid Controlled Relief Valves – BSG
- Solenoid Controlled Relief Valves – BST
- Unloading relief valves
- Check valves
- Environmental
- Valves
- Hydraulic Systems
- Power pack
- About Us
- Contact
- Blog
7 Best Aluminum Scrap Melting Furnaces for Global Buyers
Choosing an aluminum scrap melting furnace is a practical decision for recyclers, foundries, and metal processors worldwide. The right furnace affects recovery rate, energy use, melt quality, labor safety, and production consistency. A shiny ingot may look simple, but its quality begins with scrap preparation and furnace control.
Mark E. Schlesinger, author of Aluminum Recycling, has emphasized, “The value of recycled aluminum depends on careful sorting, efficient melting, and controlled processing.” This principle remains useful when comparing furnace designs. Rotary furnaces can handle mixed and contaminated scrap. Reverberatory furnaces suit larger, continuous operations. Induction furnaces offer accurate temperature control and cleaner working conditions. Electric resistance furnaces may help smaller facilities manage installation requirements.
Small details matter. Wet scrap can cause dangerous metal reactions. Excessive oxidation can reduce yield. Poorly designed charging doors may slow production and increase heat loss. These problems are easy to underestimate. I have also seen buyers focus on furnace capacity while overlooking maintenance access, burner efficiency, and local technical support.
This guide reviews seven aluminum scrap melting furnace options for global buyers. Each model should be judged by its real operating environment, not by brochure claims alone. Consider scrap composition, daily throughput, fuel availability, emissions equipment, operator skills, and planned expansion. No furnace is perfect. A technically advanced system may still perform poorly without disciplined sorting and process monitoring. The comparison ahead aims to make that choice clearer, more realistic, and easier to verify.
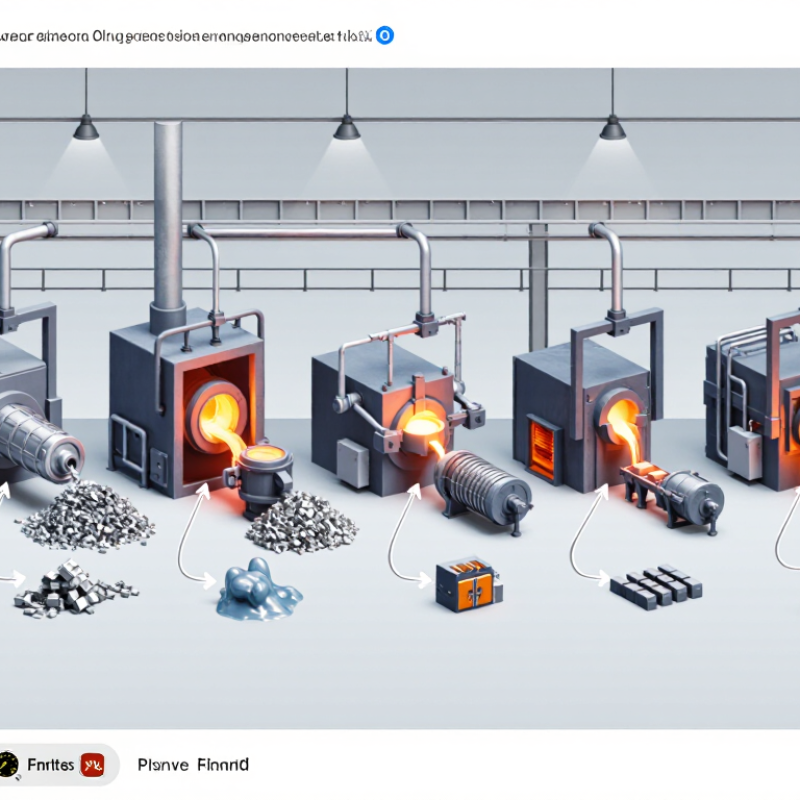
Table of Contents [Hide]
What Makes an Aluminum Scrap Melting Furnace Effective
An effective aluminum scrap melting furnace begins with predictable heat transfer. A well-insulated chamber reduces heat loss and shortens melting cycles. Electric resistance, gas, or induction heating can work well when matched to scrap volume and plant utilities. The right choice depends on energy cost, batch size, and local infrastructure.
Furnace design must also handle dirty, mixed scrap. A tilting body helps operators remove metal without excessive manual contact. A dry hearth limits moisture-related hazards and supports safer charging. Mechanical stirring or controlled circulation improves temperature uniformity. This matters when thin sheet, cast parts, and coated offcuts melt together. Reliable temperature sensors are essential. Operators should verify readings with calibrated instruments, because one failed probe can distort an entire batch.
Dross management separates a useful furnace from an expensive one. A suitable skimming system removes oxides while retaining more liquid aluminum. Sealed charging areas and effective exhaust equipment help control smoke and airborne contaminants. Maintenance access matters too. Refractory cracks, worn seals, and blocked burners rarely announce themselves early. In my practical experience, small defects often become large energy losses. No furnace is perfect. A design may perform well but still disappoint when scrap moisture, alloy variation, or operator training changes. Buyers should examine service records, spare-part access, documented safety controls, and measured fuel consumption before choosing among aluminum scrap melting furnaces.